PRODUCT KNOWLEDGE
Telecom Power System FAT Checklist: What to Test Before Shipment
Turn the approved design into witnessed factory checks for construction, electrical safety, operating states, alarms, load performance and controlled shipment release.
Updated September 14, 2026
Factory acceptance sequence
Approx. 14 minute read
What should a telecom power system FAT test?
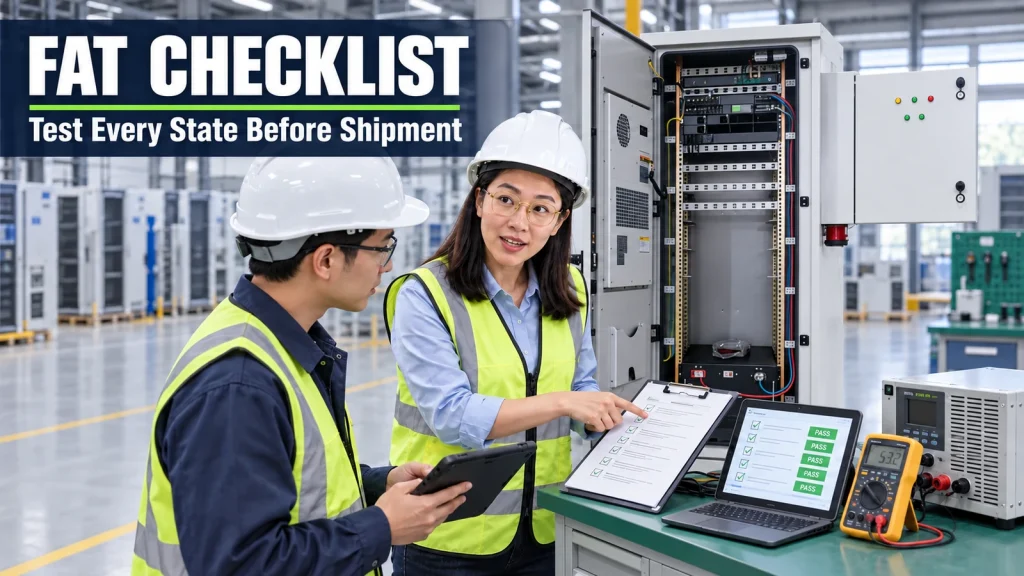 A telecom power system FAT should verify that the manufactured configuration matches the approved documents and performs the agreed normal, degraded, fault and recovery states within defined electrical, thermal and control limits. It should also prove that every result is traceable to the tested serial numbers, firmware, settings, instruments and witness record.
A useful telecom power FAT follows the actual factory integration boundary. For a rectifier plant, that boundary may include AC input, conversion, battery interface, DC distribution, controller and alarms. For an integrated hybrid cabinet, it may also include PV conversion, source switching, cooling, environmental sensors and load-shed contactors. Equipment supplied loose or installed only at site belongs in a different acceptance step.
| FAT objective |
Representative factory evidence |
What it does not prove by itself |
| Configuration conformity |
Serialised BOM, drawings, labels, firmware and settings agree with the approved release |
Suitability for an unverified site load or environment |
| Construction quality |
Mechanical inspection, wiring checks, terminal records, protective bonding and workmanship evidence |
Every type, environmental or certification test |
| Functional performance |
Energization, regulation, sharing, source transitions, battery interface and branch operation |
Performance outside the approved test boundary |
| Failure response |
Safely stimulated module, source, sensor, cooling or communication failures with recorded fallback |
Unknown failures or hazards that were not included in the procedure |
| Monitoring integrity |
Point values, alarms, timestamps, event order, protocol mapping and clear behavior |
Final carrier-network or NOC integration unless that path is available at the factory |
| Shipment release |
Closed punch list, retest evidence, approved deviations, configuration backup and packing inspection |
Correct field installation, earthing, cabling or commissioning |
The checklist must be generated from the approved power path and control narrative. A generic sheet cannot know which sources exist, which load groups are protected, which battery limits apply or which device owns a transition. Use the telecom power system component map to identify the factory boundary before assigning tests.
Factory acceptance is not product certification
FAT is a project and contract acceptance activity. It confirms the supplied configuration against agreed requirements; it does not create certification, replace a required design verification or authorize a test outside the laboratory, product-standard or conformity-assessment scope.
This distinction matters when a test name appears in both production and compliance documents. IEC 62911:2025, corrected in June 2026, defines routine electrical safety testing used during or after manufacturing for equipment within its scope. The IEC description explicitly separates tests intended to detect manufacturing errors from product development or verification. Apply it only where the tested equipment and conformity scheme fall within that scope.
Likewise, IEC 61439-1:2020 provides general rules and verification requirements for low-voltage switchgear and controlgear assemblies. It is used with the applicable assembly part, and incorporated converters still rely on their relevant product standards. A telecom cabinet containing breakers does not automatically make every function inside it compliant with the complete IEC 61439 series.
Do not improvise high-energy tests
Dielectric, insulation, fault, battery and protection tests must follow the approved method, equipment limitations and safety controls. Isolate or configure sensitive electronics, surge-protection devices, batteries and communication circuits exactly as the released procedure requires. A witnessed FAT is not permission to defeat interlocks or exceed ratings.
Freeze the test basis before the witness date
The FAT begins when the supplier and buyer agree what will be tested, not when power is switched on. Freeze the offered scope, applicable document revisions, test configuration, simulated interfaces, witness points, responsibilities, instruments, pass criteria and evidence format before the equipment occupies the test bay.
Effective factory acceptance testing needs a controlled baseline that contains:
- approved single-line diagram, wiring drawings, cabinet layout, cable and terminal schedules;
- released BOM with manufacturer, model, option, rating, quantity and serial-number requirement;
- source, converter, battery, distribution, load and cooling operating limits;
- controller firmware, parameter file, protection settings, alarm matrix and interface maps;
- normal, degraded, fault, recovery, maintenance and communication-loss state descriptions;
- test supply capacity, load-bank arrangement, battery simulator or approved battery configuration;
- instrument ranges, accuracy, calibration status and connection points;
- hold, witness and review points plus the authority allowed to accept deviations;
- safety plan, isolation method, emergency response and test-area responsibilities;
- record templates for raw readings, screenshots, event logs, photographs, exceptions and signatures.
Issue the procedure early enough for review. Discovering on witness day that the factory supply cannot reproduce the specified input, the load bank cannot reach the duty point or the buyer expects a test that could damage connected electronics creates pressure to accept weak substitutes. Record every limitation and agree an alternative method or a later test stage before execution.
How should FAT pass criteria be written?
Write each pass criterion as an observable result tied to a stimulus, test condition, measurement point, tolerance or allowed state, response time where relevant and retained record. “System works,” “alarm normal” and “voltage OK” are observations, not acceptance criteria.
| Procedure field |
Required content |
Weak wording to reject |
| Precondition |
Document revision, configuration, source condition, load, battery state, temperature and active overrides |
Unit ready |
| Stimulus |
Exact command, simulated signal, source change or safely isolated component |
Create a fault |
| Measurement |
Named terminals, meter or controller point, unit, sample method and timestamp |
Check voltage |
| Expected sequence |
State change, delay, command, feedback, alarm and recovery order |
Transfer is normal |
| Pass limit |
Approved range, maximum interruption, required state, tolerance or zero-defect visual condition |
Acceptable |
| Evidence |
Reading, trace, event log, image, configuration checksum, witness initials and exception ID |
Passed |
For example, a bus-voltage test should name the supply condition, load level, battery condition, controller mode and terminals at which voltage is measured. The pass band must come from the approved load interface and power-system design rather than a universal nominal value. If the result is read from the controller, compare it with an appropriate reference instrument and record both values.
Give each test a unique ID and link it back to one or more requirements. That traceability prevents a long power system checklist from hiding an untested contract clause. It also lets the final report show which requirements passed, failed, were accepted by document review or remain reserved for the site.
Which checks belong before first energization?
Before energization, confirm identity, construction, isolation, wiring, protective paths and test readiness. No powered test should begin while the as-built circuit differs from the released drawing, temporary workshop wiring is undocumented or the test supply and load bank exceed the approved connection arrangement.
- Identify the unit. Record project, assembly designation, serial numbers, ratings, destination configuration and drawing revisions.
- Reconcile the BOM. Compare installed models, quantities, options, firmware-capable hardware and supplied loose items with the approved release.
- Inspect construction. Check dimensions, doors, locks, hinges, seals, panels, rack positions, service access, lifting features and shipping restraints against the drawings.
- Inspect wiring. Trace conductor origin and destination, size or identification, separation, routing, bend support, abrasion protection, terminal markers and polarity conventions.
- Review connections. Verify the approved torque process and retained records for current-carrying and protective connections; do not substitute a paint mark for the torque method.
- Confirm protection and isolation. Match devices, settings, fuse links, disconnects, interlocks and labels with the approved schedules.
- Verify protective bonding. Test the defined metal parts and doors using the applicable method, instrument and pass limit; inspect earth studs and bonding conductors.
- Perform approved electrical safety checks. Apply continuity, insulation or dielectric procedures only to the circuits and states for which they were released.
- Check auxiliaries. Inspect fans, filters, air conditioners, heaters, drains, lights, sockets, sensors and cable-entry provisions included in the factory scope.
- Clear temporary conditions. Document test leads, bypasses, simulated inputs and workshop supplies so none can be mistaken for the final configuration.
Photograph exceptions before they are corrected and preserve the original finding. A clean final image without the punch-list history cannot prove that the defect was evaluated, repaired and retested.
Establish a controlled powered baseline
First energization should prove that the assembly enters a known safe state before the procedure introduces transitions or failures. Start with the approved source, limited test load and defined battery condition. Confirm polarity, phase arrangement where applicable, source values, controller boot, active limits, protective-device state and absence of unexpected alarms.
Increase load through the planned steps while recording input, bus, branch and battery measurements at named points. Verify converter start and stop, module discovery, current sharing, regulation, current limiting where safely testable, redundant capacity status and controller readings. The telecom rectifier system guide owns rectifier capacity and redundancy design; FAT confirms the released plant performs that design under the agreed test cases.
Check every populated load branch and every authorized spare way. Operate the protective device or test mechanism by its approved method, confirm branch identity and returned state, and verify that a healthy branch remains in the intended state. Record voltage at the distribution point and, where the factory scope includes representative load cabling, at the load interface.
Measure the test boundary
A load-bank display can confirm its own demand but not the voltage, current or loss at every upstream interface. Record the source input, converter output, battery branch and selected load terminals required by the procedure, using synchronized timestamps where transition behavior matters.
Which operating and failure states should the FAT exercise?
Exercise every state that the factory-integrated equipment is required to detect, enter, control and leave. At minimum, test normal supply, loss of the preferred source, reserve operation, controlled load shedding, degraded converter capacity, relevant auxiliary failures, communication loss and source recovery when those functions exist in the approved configuration.
| State or event |
What to stimulate safely |
Evidence to retain |
| Normal source available |
Approved input and representative load with defined charging permission |
Source, bus, load and battery values; module states; normal alarms |
| Preferred source lost |
Approved source-removal method or qualified simulator command |
Detection time, lowest load-interface voltage, retained loads, alarm and state transition |
| Low reserve or battery restriction |
Simulator, controlled setpoint or approved battery/BMS test function |
Charge/discharge limit, contactor or LVD response, load-shed order and recovery rule |
| One converter unavailable |
Approved module isolation or removal at the specified load state |
Remaining capacity, sharing, bus response, redundancy alarm and replacement behavior |
| Cooling or sensor failure |
Approved fan, cooling command or sensor simulation |
Alarm delay, fallback action, active thermal limit and clear condition |
| Controller or communications loss |
Defined local link, gateway or supervisory path interruption |
Local protective state, stale-data behavior, alarm, command block and reconciliation after return |
| Source recovery |
Restore an input inside the qualification window |
Stability delay, transfer, recharge ramp, staged load restoration and anti-cycling behavior |
| Maintenance isolation |
Operate the designated safe isolation boundary |
Affected circuits, healthy circuits, physical indication, remote state and return-to-service sequence |
The test method should create the signal or condition without creating an uncontrolled hazard. Do not deep-discharge a lithium battery merely to reach a low-reserve alarm when a validated simulator or controlled test input can prove the logic. Do not short a branch to demonstrate a protection setting unless the approved test facility, device method, risk assessment and instrumentation are specifically designed for that energy.
Each transition in the FAT test procedure should record the state before the event, the initiating input, detection delay, commanded output, actuator feedback, alarm timestamp, final state and recovery. A pass requires the correct sequence, not just the correct final screen.
Prove load, redundancy and thermal duty together
Electrical output and thermal behavior should be tested in the same populated configuration when practical because converter loss, charging, cable heating and cooling duty interact. The FAT plan must state the test load, duration, ambient condition, cabinet state and whether the result represents steady operation or only a time-limited functional check.
Test the agreed normal duty, recovery or recharge duty, growth case and degraded capacity case that can be reproduced safely at the factory. Verify that reserved converter capacity remains real after environmental derating and that a module failure does not force the remaining units beyond their approved loading. Record current sharing, internal temperatures, controller limits and cooling input over time.
A workshop thermal run does not automatically reproduce outdoor solar gain, extreme ambient temperature, altitude, wind, dust loading or completed field cable entries. If those conditions are not reproduced, connect the FAT record to the applicable design calculations, product evidence or environmental tests and reserve final installation effects for SAT. The telecom cabinet cooling guide explains the wider thermal evidence boundary.
Trace every required alarm from stimulus to record
Monitoring acceptance should prove the complete factory-available path from physical or simulated condition to local value, alarm, event log and communication interface. It should also prove the clear sequence and distinguish a failed sensor or communication path from a normal reading.
For each required point, verify asset identity, source channel, value or state, engineering unit, scaling, timestamp, quality, severity, delay, latching, acknowledgement and clearance. Compare important measurements with a suitable reference. Restart the controller or gateway, interrupt the approved communication link, restore it and confirm that configuration, buffered records and current state recover as specified.
The dedicated SNMP, Modbus and dry-contact guide owns protocol-specific mapping tests. The broader telecom site monitoring guide owns sensor-to-NOC architecture. This FAT checklist confirms only the points and paths included in the factory witness boundary.
Keep factory and site acceptance boundaries separate
FAT should close the risks that can be controlled at the factory; SAT should verify interfaces created by transport, installation and the real site. Repeating every factory step at site wastes access time, while moving a factory-controllable defect to SAT makes correction slower and more expensive.
| Normally strongest at FAT |
Normally strongest at SAT |
| BOM, serial numbers, internal wiring, firmware, settings and factory workmanship |
Foundation, mounting, field cable entry, final clearances and transport condition |
| Controlled source, load-bank, battery-interface and failure simulations |
Actual utility, generator, PV array, battery bank and telecom loads |
| Integrated cabinet control, branch, cooling and local alarm functions |
Site earthing and bonding network, surge interfaces and external protective coordination |
| Factory gateway, protocol and point-map verification |
End-to-end backhaul, firewall, NOC routing, time synchronization and operator workflow |
| Configuration backup, drawings, manuals and packing readiness |
As-installed redlines, commissioning baselines, training and operations handover |
Some projects can extend the factory witness through a secure remote NOC connection or use a full source and battery emulator. Others cannot. State the actual boundary rather than awarding a pass for an interface that was never connected.
What evidence is required before shipment release?
Shipment release requires a signed result for every planned test, disposition and retest evidence for every exception, and a frozen record of the exact hardware and configuration being packed. An unresolved safety, functional or interface defect should not disappear into a general “open items” note.
Complete shipment release evidence should contain:
- approved FAT procedure, attendance record and completed requirement-to-test matrix;
- tested assembly identifiers, installed serial numbers, BOM and drawing revisions;
- firmware, parameter, protection-setting and communication-map backups with revision or checksum;
- test instruments, ranges, calibration status and connection arrangements;
- raw readings, load profiles, transition traces, controller logs, alarm/event exports and selected photographs;
- each nonconformance, technical disposition, authorized acceptance, correction and witnessed retest;
- approved concessions separated from items that must close before shipment;
- as-built redlines, manuals, spare parts, tools, keys, loose-supply items and packing list;
- transport restraints, battery shipping state where applicable, moisture protection, cabinet closure and external package inspection;
- remaining SAT tests, site prerequisites, responsible party and required commissioning records.
Close the report with a release statement that names the accepted serial numbers and the exact configuration. If firmware, settings, wiring, equipment or protection changes after the witnessed test, identify the affected test cases and repeat them before the new configuration is released.
Project boundary
This checklist is a method for preparing a project-specific FAT. It does not prescribe universal voltage limits, protection settings, test currents, thermal limits, battery conditions, witness points or certification requirements. The approved design, equipment instructions, applicable standards, destination rules and risk controls remain authoritative.
Turn the approved power design into a witnessed FAT
Send the system architecture, load and source cases, battery interface, control narrative, alarm map, drawings, applicable standards and required witness points. Huijue can help organize them into a configuration-specific FAT procedure and evidence schedule.
Submit the FAT inputs